 EN
Global distributors face constant pressure to source reliable, high-performance products that meet diverse market demands across regions. When it comes to travel case selection, purchasing leaders and logistics managers evaluate dozens of factors before committing to a partnership. Our travel case line has earned consistent preference among global distributors because it delivers on the core requirements that matter most: durability, security, capacity, and value alignment with end-user expectations.
Choosing the right travel case supplier is not a simple procurement decision. Distributors operate in competitive markets where product quality directly influences customer satisfaction, return rates, and brand reputation. Our travel case line stands out because it addresses the real operational challenges that distributors and end-users experience: damage during transit, security concerns, capacity limitations, and the need for professional appearance across business and leisure travel contexts.
Superior Build Quality and Durability Standards
Reinforced Construction for Extended Lifecycle
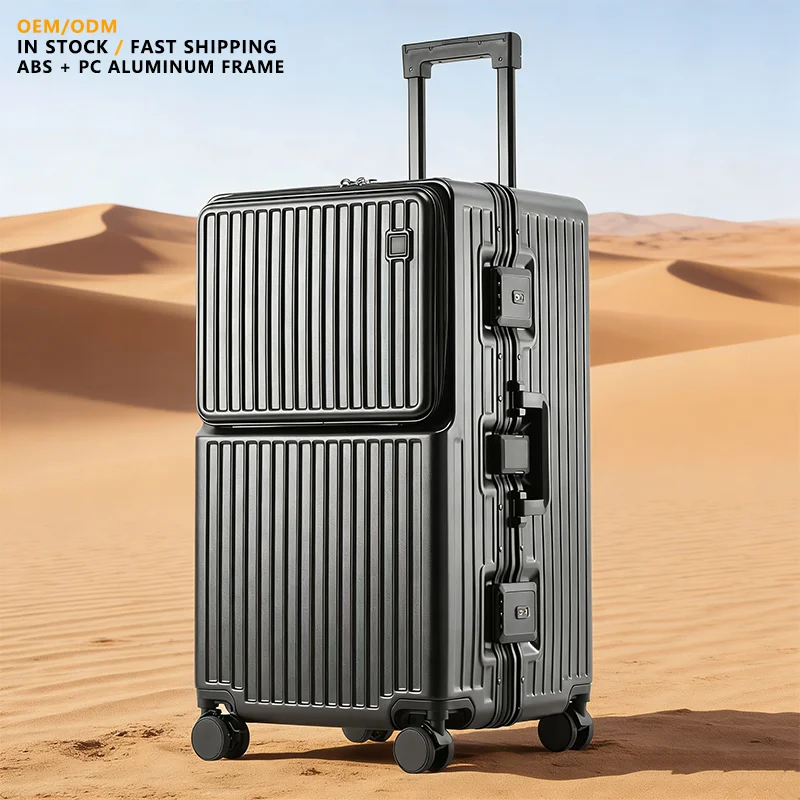
The foundation of distributor preference for our travel case begins with construction integrity. Our travel case line features reinforced aluminum frame architecture combined with high-grade polycarbonate shells designed to withstand repeated transit cycles, baggage handling impacts, and varying climate conditions. This reinforced approach extends the product lifecycle significantly, reducing replacement frequency and customer dissatisfaction claims that typically consume distributor resources and margin.
Distributors recognize that a travel case failing mid-season creates customer service burdens, warranty claims, and relationship damage that far exceed the initial product margin. Our travel case construction philosophy prioritizes reliability over cost minimization, which resonates strongly with distributors who prioritize customer retention over short-term margin extraction. The reinforced frame structure prevents the common failure points observed in competing travel case products, such as corner cracking, hinge separation, and handle fracture under normal use conditions.
Material Selection and Testing Standards
Every travel case in our line undergoes rigorous material testing and quality verification before shipment. We source premium polycarbonate compounds that resist UV degradation, temperature fluctuations, and impact stress that would compromise lesser travel case materials. Distributors appreciate this attention to material science because it translates directly into lower product return rates, fewer customer complaints, and stronger profit margins per unit sold.
Our travel case testing protocols exceed industry baseline standards, including drop testing, stress testing, and environmental chamber exposure. This commitment to quality assurance means distributors can confidently represent our travel case line to their retail partners and corporate clients without concern for premature failure or quality inconsistency across production batches.
Advanced Security Features and Customer Confidence
Anti-Theft Design and Access Control
Security ranks among the top distributor selection criteria when evaluating travel case suppliers. Our travel case line incorporates anti-theft password lock systems, reinforced zipper construction, and TSA-compliant designs that provide both physical protection and psychological confidence for business travelers. Distributors recognize that a travel case with comprehensive security features commands higher customer willingness to pay and generates positive word-of-mouth recommendations that fuel repeat orders.
Business travelers increasingly demand travel case solutions that protect valuable equipment, documents, and personal items during airport transit and hotel storage. Our travel case addresses this market demand through integrated security architecture that becomes a key selling point in distributor pitch conversations with corporate procurement teams and travel management companies.
Professional Appearance and Brand Alignment
Beyond functional security, our travel case line projects professionalism and reliability through visual design and finish quality. Distributors understand that business travelers judge travel case products not only by utility but by aesthetic alignment with corporate image standards. Our travel case designs incorporate clean lines, premium color options, and refined hardware finishes that satisfy executive-level expectations and corporate travel policies.
This aesthetic positioning enables distributors to sell our travel case line into higher-value market segments, including executive gift programs, corporate travel budgets, and premium hospitality applications where appearance quality directly influences purchase decisions and perceived value.
Capacity Efficiency and Practical Design Elements
Spacious Interior Architecture and Packing Optimization
Practical capacity represents a critical distributor evaluation factor because it directly addresses end-user frustration with undersized travel case products. Our travel case line delivers generous interior volume through optimized dimensional engineering that maximizes usable space while maintaining structural integrity and weight management. The 28-inch dimension option, combined with reinforced wall thickness and strategic interior organization, enables business and leisure travelers to pack more efficiently than competing travel case offerings in similar price ranges.
Distributors consistently report that capacity satisfaction drives positive customer feedback and repeat purchases of our travel case line. When end-users experience a travel case that genuinely accommodates their packing requirements without overstuffing or damage risk, they become reliable repeat customers who influence others within their professional networks and social circles.
Front-Open Access and Convenience Features
Our travel case design includes front-access compartments and internal organization features that simplify packing and retrieval workflows. Distributors understand that convenience features distinguish premium travel case products from commodity alternatives. Business travelers particularly value the front-open travel case configuration because it enables quick access to frequently needed items during airport transitions and layovers without full luggage opening.
This practical design philosophy translates into distributor marketing advantages. When sales teams can demonstrate our travel case with fully operational front access and compartmented organization, they communicate tangible product intelligence that justifies premium positioning and influences purchase decisions among discerning business customers.
FAQ
What makes our travel case line preferable to standard luggage alternatives?
Our travel case incorporates reinforced construction, advanced security features, and practical design elements specifically engineered for business and frequent travelers. Standard luggage often prioritizes cost minimization over durability and security, resulting in higher failure rates and customer dissatisfaction. Distributors prefer our travel case because it delivers measurable quality differentiation that justifies margin structure and builds customer loyalty through superior performance.
How does our travel case compare to competing premium travel case brands?
Our travel case stands out through balanced emphasis on durability, security, and aesthetic professionalism at price points that enable distributor margin optimization. We focus on engineering excellence and material quality rather than exclusive brand positioning, making our travel case accessible to broader customer segments while maintaining premium perception. Distributors value this strategic positioning because it expands addressable markets without requiring premium pricing that limits volume potential.
Can distributors customize our travel case line for corporate branding applications?
Our travel case platform supports customization options including color selection, logo embroidery, and branded packaging solutions that enable distributors to create differentiated product offerings for corporate clients. This customization capability transforms our travel case from commodity product into branded corporate gift solutions that command higher margins and strengthen client relationship value for distributor partners.